by Sara McCaslin Sara McCaslin No Comments

What Makes ePTFE Sheet Different and When to Specify It Over Standard PTFE

Many flange gasket failures trace back to a few root causes: inadequate chemical compatibility, poor conformability to the flange face, or gradual loss of sealing force through creep. Standard PTFE sheet addresses these challenges only partially. Filled formulations introduce a problematic contamination risk in ultra-pure applications, while unfilled skived PTFE often struggles to conform to rougher or damaged sealing surfaces.

ePTFE sheet was developed to close these gaps. Made from 100% PTFE with no fillers, it expands into a multi-directional microfibril structure that delivers significantly greater flexibility and creep resistance than standard PTFE sheet, without compromising chemical or thermal performance. The sections that follow examine the properties behind this performance and the applications where ePTFE sheet is most commonly specified.

What Makes ePTFE Sheet Different from Standard PTFE

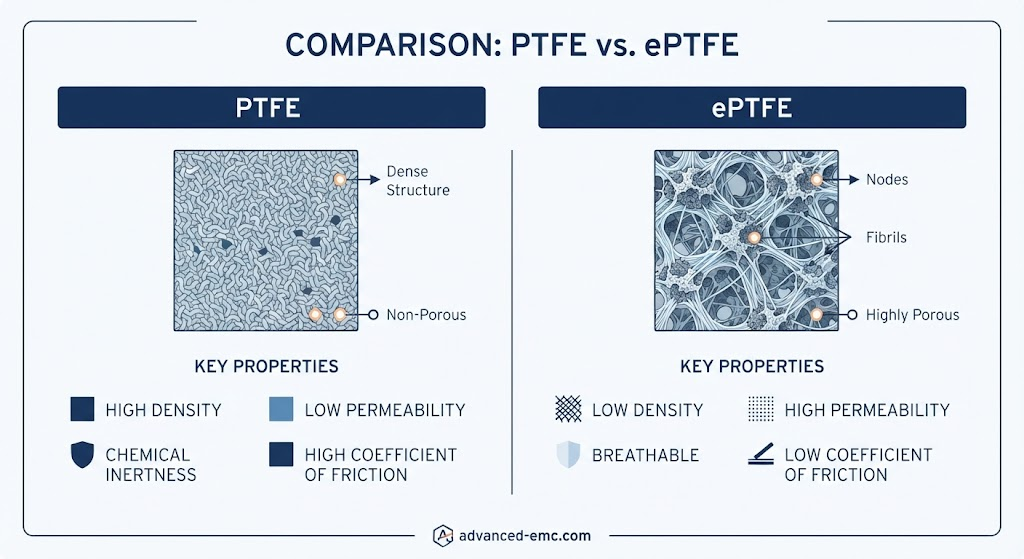
ePTFE sheet is made from 100% PTFE with no fillers and expanded through a special process into a multi-directional microfibril structure. Its interconnected node-and-fibril structure, illustrated below, creates a highly compressible material that can conform to flange-face irregularities while maintaining useful tensile strength and improved resistance to cold flow. The result is a PTFE sheet with strong creep resistance that is also easy to cut and fabricate on site. 
Key Performance Properties

What follows are some of the key properties of ePTFE sheet:

  • Temperature range: -286°C to 270°C (-450°F to 518°F), making it a good choice over a wide range of temperatures
  • pH range 0–14 (chemical resistance)
  • Tensile strength >20 MPa
  • Stress retention of 15 MPa
  • Specific leakage rate 2.6×10⁻⁷
  • Compressibility 45% / recovery 14% (ASTM F36M)
  • Bonus properties: hydrophobic, low friction coefficient, UV resistant

It also has PTFE’s chemical inertness and extremely low coefficient of friction. It is also hydrophobic and UV resistant.

Benefits of ePTFE Sheet

ePTFE sheet is low-friction, non-stick, chemically inert, and exhibits good strength. It also offers excellent extreme-temperature reliability and high dielectric strength. These sheets are strongly hydrophobic, provide good electrical insulation properties, and can handle long-term exposure to UV as well as harsh outdoor conditions. Certain virgin-PTFE materials may be suitable for food-contact or pharmaceutical applications when supported by the supplier’s applicable FDA and compliance documentation. ePTFE’s resistance to creep and deformation under load leads to good dimensional stability.

Drawbacks of ePTFE

As with any material, ePTFE has drawbacks. These include its cost, mainly due to its manufacturing process and the fact that PTFE is a high-performance polymer. However, that cost is often justified because no other feasible solution may exist. ePTFE is primarily a static-sealing material. As such, it is generally not the preferred choice for applications requiring high abrasion resistance, dynamic sliding wear resistance, or high mechanical recovery. Repeated thermal cycling can cause dimensional changes that affect performance. Finally, ePTFE does not work well with molten alkali metals such as lithium and concentrated sodium.

Where ePTFE Sheet Gets Specified

In oil and gas applications, ePTFE sheet is most commonly used at flange connections. Its chemical resistance across a pH range of 0–14, combined with a 200 bar pressure rating, makes it an excellent option for static sealing across a broad range of process media, including aggressive hydrocarbons and treatment chemicals.

Pharmaceutical and medical applications have different requirements. Because ePTFE contains no fillers, it is well suited to glass-lined flange seals and sanitary sealing points, where product purity cannot be compromised by leaching or contamination, which is a common limitation of filled gasket materials in these environments.

In chemical processing, ePTFE sheet is used for valve and pump static seals. Its chemical inertness and strong creep resistance help maintain sealing force through repeated thermal cycling and exposure to corrosive media. ePTFE is also used for analytical instrument seals, research equipment that requires chemical compatibility, and laboratory glassware components.

Pulp and paper operations rely on ePTFE sheet for maintenance hole cover gaskets. Its conformability compensates for the slightly irregular or worn sealing surfaces typical of large access covers, reducing the need for tighter machining tolerances.

Food processing and pharmaceutical facilities both specify ePTFE sheet for mixers and similar equipment, where its purity profile and resistance to cleaning chemicals support the frequent washdown cycles required in food-grade environments. 

The semiconductor industry uses ePTFE sheets in ultra-high purity applications, process chamber seals, and chemical delivery systems.

Conclusion

ePTFE sheet provides a practical solution for many static sealing applications where conventional PTFE may struggle with flange irregularities, low available bolt load, or long-term creep resistance. Its filler-free construction, chemical compatibility, and high conformability make it well suited to demanding process environments. To discuss the right sheet grade, thickness, and gasket configuration for your application, visit our ePTFE Products page or Request a Quote today. 
by Sara McCaslin Sara McCaslin No Comments

PTFE Auto Molding vs. Machining: When Compression Molding Is the Better Manufacturing Route

Auto molding and machining are are different manufacturing processes that both lead to a finished part. Which option is better depends on part design, production volume, material, critical dimensions, tolerance requirements, production economics, and the equipment in which the part will operate.

In this article, we look specifically at PTFE auto moding and machining to discuss when auto molding is the better manufacturing option.

What Is PTFE Auto Molding?

Auto molding, also known as compression molding, uses heated compression and dies to form a near-net-shape polymer part. It is a commonly used manufacturing technique for making thermoset and thermoplastic parts,  as well as rubber and composites. It is also one of the oldest plastic forming methods still in use. 

The auto molding process starts by placing a pre-measured amount of material (usually in the form of a preheated plug, sheet, or granules) into an open, heated mold cavity. That mold is then closed with a matching upper half. A hydraulic press is used to apply high pressure that forces the material to fill the entire cavity shape. 

The combination of heat (typically 250–400°F depending on the material) and pressure causes the material to cure (or vulcanize). The result is permanent cross-links within the PTFE polymer structure that lock it into the desired shape. For compression molding PTFE compounds, pressure, sintering temperature, and dwell time are critical process variables. Typical molding pressures of 3,000–4,500 psi and sintering temperatures in the 685–720 °F range are required, while the dwell time is dependent on part geometry, volume, and machine capability.

Once curing is complete, which can take anywhere from a minute to several minutes depending on part thickness and material, the mold opens and the finished part is ejected. Auto molded parts often require minimal trimming of excess flash material. 

What PTFE Machining Does Well

An alternative manufacturing method often used with PTFE is machining. Machining removes excess material to produce the final part and may include processes such as milling, turning, and drilling. This approach is well adapted to situations that involve …

  • Prototype and development parts
  • Low-volume production
  • Designs that are still changing
  • Components with highly localized geometry or features
  • Parts requiring final sizing, precision finishing, or secondary features after molding
  • Jobs where a dedicated mold is not economically justified

A part’s complexity, stock availability, scrap rate, and tolerance demands all impact the cost of machining PTFE parts.

Where Auto Molding Excels Over Machining

There are, however, several benefits to auto molding. For example, near-net-shape production can reduce material removal and tooling can make sense when demand is stable and sufficient. Auto molding is also a  repeatable molding process can support recurring production. 

And thick, large, or geometry-specific parts may benefit from being formed closer to finished shape. In addition, molding can reduce subsequent machining, though some finishing may still be required (e.g.,  machining, facing, drilling, or other finishing operations. Finally, material and process control can be tailored to the specific PTFE compound and part geometry

What are the Real Decision Factors

The table below summarizes the decision factors that are involved.

PTFE Auto Molding vs. Machining: Decision Matrix

Decision Factor PTFE Auto Molding Favored When Machining Favored When
Production Demand The part is recurring, and annual demand supports tooling economics. Demand is low, uncertain, or one-time.
Geometry Near-net-shape tooling can form much of the required profile. Geometry changes frequently or needs flexible revision.
Material Utilization Starting from stock would create substantial removed material. Stock shape is already efficient for the design.
Lead Time Tooling exists or production is repeatable after tool qualification. A part is needed before a tool can be designed and qualified.
Tolerances The molded shape can meet requirements with limited finishing. Tight, localized, or feature-specific tolerances dominate.
Secondary Operations The design can be completed with minimal post-mold work. Numerous holes, threads, grooves, or custom features are required.
Design Maturity The drawing, material, and demand forecast are stable. The part remains in prototype or iterative design stages.

PTFE Compound Selection Is Part of the Auto Molding Process Decision

Keep in mind that unfilled PTFE and filled PTFE compounds should not be treated as interchangeable. For example, fillers can impact properties such as wear resistance, stiffness, thermal behavior, electrical behavior, friction, and process response. The compound selected should account for factors such as pressure, sliding speed, counterface, media, temperature, chemical exposure, contamination, and dimensional requirements. A manufacturing route should be selected after the material and functional design are understood, not before.

What to Send a PTFE Auto Molder

Here is the type of information that a PTFE molder would need to provide a quote:

  • Part drawing and revision level
  • 3D model if available
  • Material specification or functional requirements
  • Critical dimensions and GD&T (Geometric Dimensioning and Tolerancing)
  • Tolerances required after sintering and any machining
  • Service temperature, pressure, media, and load conditions
  • Counterface materials and surface finish for bearing or sealing components
  • Regulatory, traceability, inspection, or documentation requirements
  • Whether the part is a prototype, bridge-production part, or long-term production design

Conclusion

PTFE auto molding shapes near-net parts under heat and pressure, which both cuts waste and machining time versus starting from stock. Auto molding is the smart choice for recurring, stable-volume production where the molded shape can meet tolerances with minimal finishing; machining, however, is till the preferred choice for prototypes, low-volume runs, or tight localized features.

Not sure which route best fits your part? Send Advanced EMC your drawing, material spec, critical dimensions, and production volume, and our team will help you find the most cost-effective path from design to finished part.