by Sara McCaslin Sara McCaslin No Comments

Spring-Energized Seal Energizers: How to Choose the Right One, Part 1

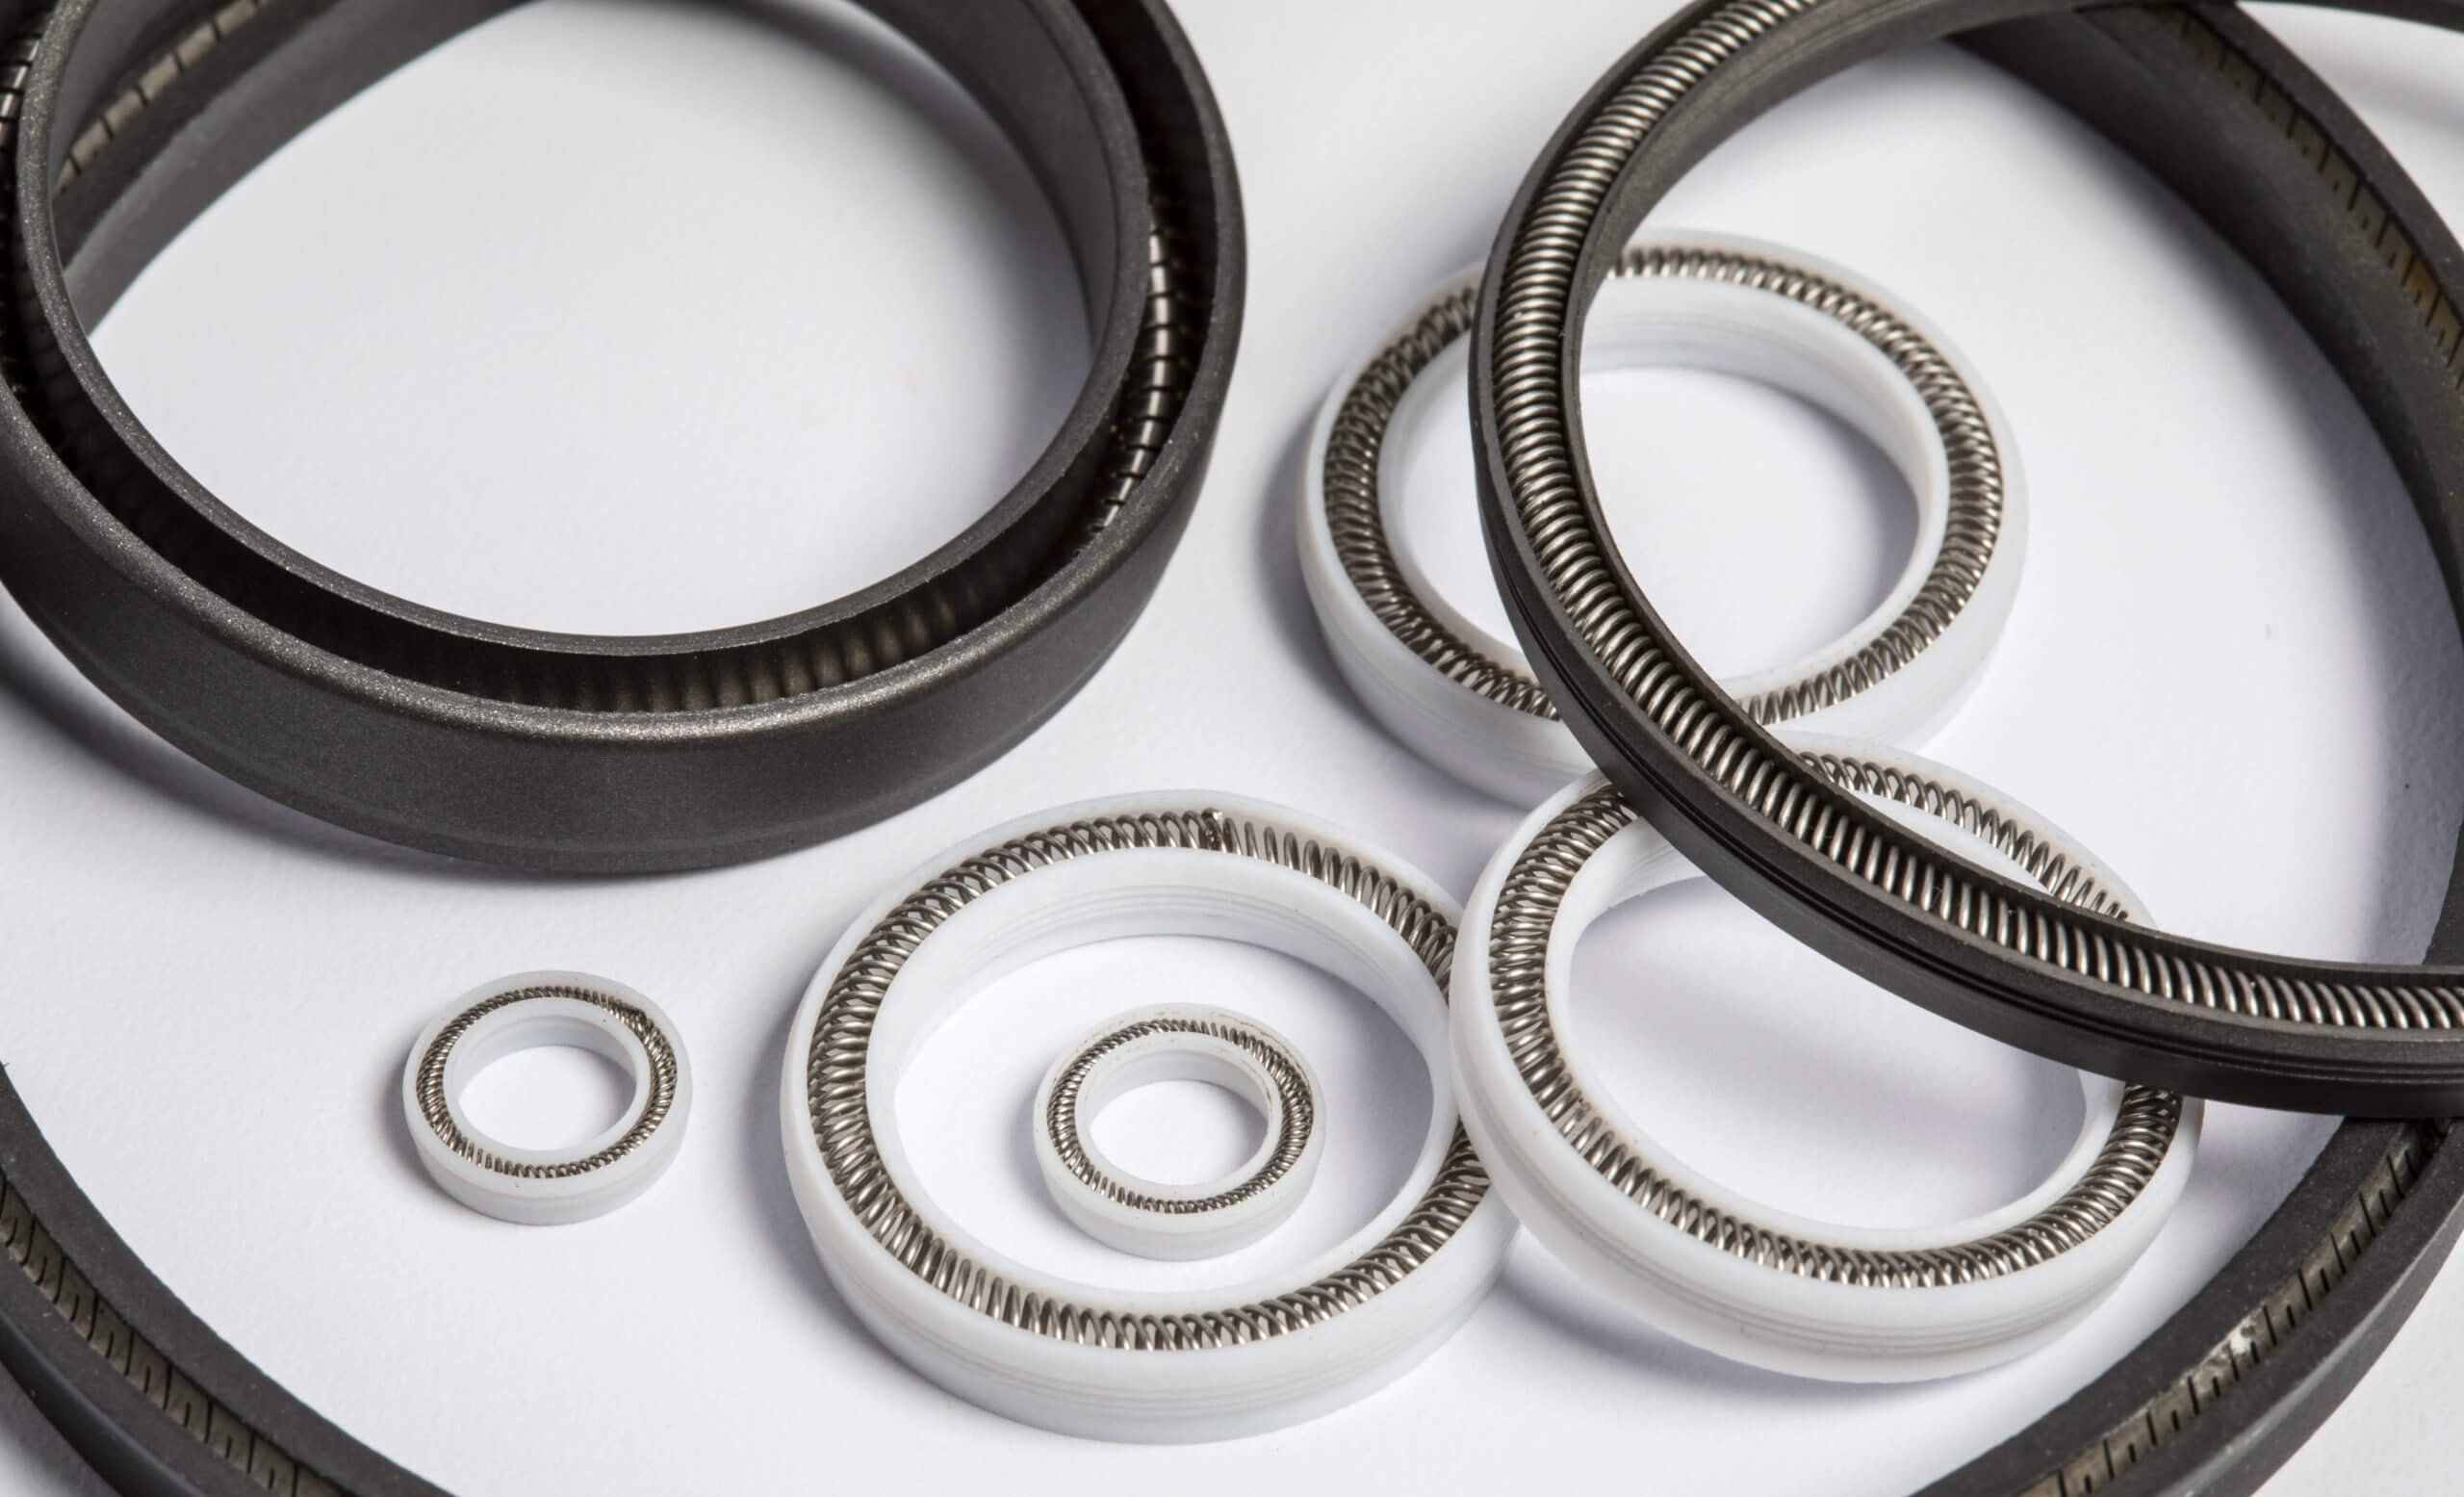
One challenge of working with PTFE and other polymer seal jackets is their poor elastic memory. Spring energizers address this challenge by providing the consistent sealing force required.  However, choosing an energizer means trading off load, deflection range, friction, and leak tightness. This article presents a practical selection framework for selecting the right spring energizer.

What the Spring Energizer Actually Does
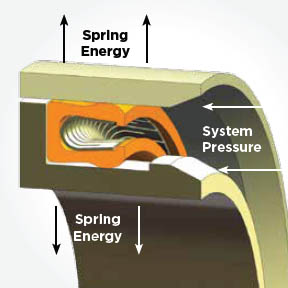
A spring energizer keeps the seal lip in contact even at low or zero system pressure. It effectively mitigates issues related to jacket creep, thermal contraction/expansion, and hardware tolerances over the life of the seal. As system pressure rises, fluid pressure pushes the seal lip outward and takes on more of the sealing load. In fact, the spring has the most significant impact at low pressures, vacuum conditions, and system startup. The spring energizer sets the baseline contact stress, while application requirements determine whether this minimum threshold is adequate. 

The Three Spring Properties That Drive Selection

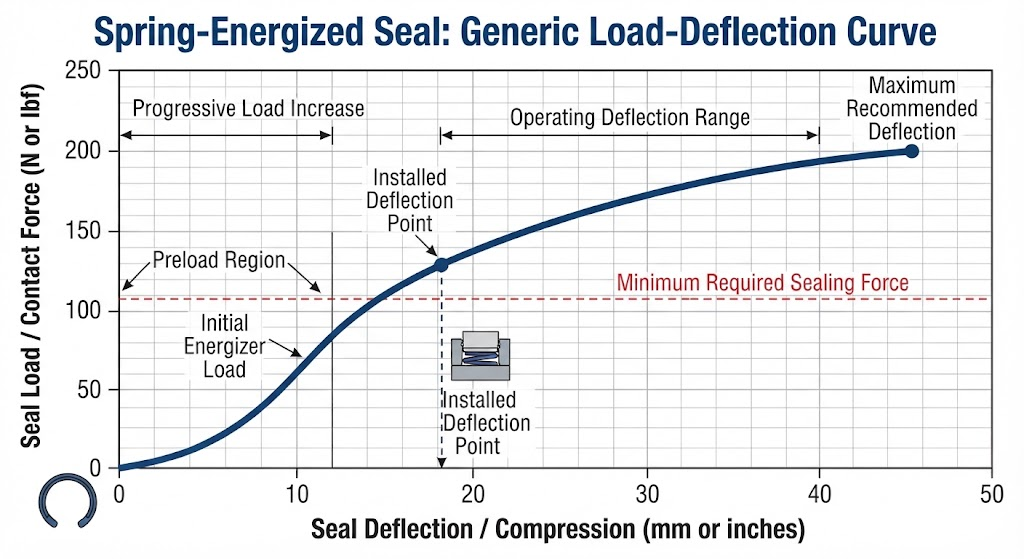
Three spring properties are critical to spring energizer selection: load, load-deflection curve, and where the load lands. 

Load (Unit Load)

The load, or unit load, is the contact force per unit of circumference. Higher loads give better leak tightness at low pressure but lead to more friction and wear.

Load-Deflection Curve

The load-deflection curve shows how much the load changes as the spring compresses. This determines how well the seal handles tolerance issues, eccentricity, and wear.
Where the Load Lands

The load can be concentrated at the lip tip or spread along the lip. This affects scraping, friction, and gas tightness.

Cantilever (V) Spring Energizers

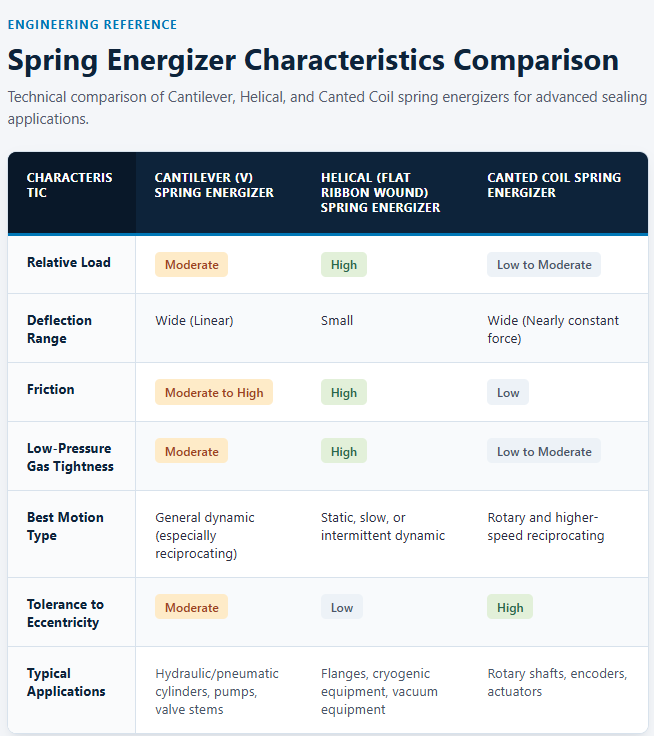
Cantilever spring energizers, also called V springs, are formed from a metal strip that has a V-shaped cross section. In this design, the load is concentrated near the front of the seal lip. 

This type of spring energizer can handle a moderate load with a roughly linear load-deflection curve across a wide range. These spring energizers are good in general dynamic service, especially when it involves reciprocating motion. They also work well for scraping and excluding contamination and offer a good cost-to-performance ratio. Cantilever spring energizers are commonly used with hydraulic and pneumatic cylinders, pumps, and valve stems.

Cantilever spring energized seals do have limitations: (1) friction is going to be higher than in canted coil spring energizers, and (2) the open cavity can trap media.

Helical (Flat Ribbon Wound) Spring Energizers

Helical spring energizers are composed of a continuous wound ribbon that supports the full circumference of the lip. They can carry the highest load and have a steep load-deflection curve, meaning they have only a small usable deflection range. Helical spring energized seals offer the tightest seal at low pressure, in vacuum, and against light gases (helium, hydrogen). 

Helical spring energized seals are typically found in static and slow or intermittent dynamic service, in flanges, and in cryogenic and vacuum equipment. However, the high load pushes the jacket into surface irregularities, which can tighten the seal but increase friction and wear in dynamic service. In addition, they are less tolerant of hardware tolerances and eccentricity.

Canted Coil Spring Energizers

Canted coil spring energizers are round wire coils wound at an angle, and each coil deflects at the same time when compressed. This creates a nearly constant force over a wide deflection range, which is often why canted coil springs are chosen. They exhibit low, stable friction and tolerate wear, tolerances, and eccentricity. In addition, canted coil spring energizers are well suited to rotary and higher-speed reciprocating service. They are used in applications where friction or torque must remain steady, as well as in rotary shafts, encoders, and actuators.

Canted coil spring energizers can typically handle a lower unit load than helical, so they tend to be less leak-tight in low-pressure gas or vacuum. In addition, abrasive media can damage the lips and cavity. 

Side-by-Side Comparison

The table below compares the three spring types discussed in terms of key seal properties.
Spring Material Selection

Common spring options include 301-series stainless steel, Elgiloy® (a cobalt-chromium-nickel alloy), Hastelloy® C-276, and Inconel®. Experts recommend choosing the material based on factors such as corrosion, sour-service (NACE MR0175/ISO 15156) requirements, temperature, and relaxation resistance.

Conclusion

Each type of spring energizer has its own features and applications for which it is well adapted. To learn more about selecting the right one for your application, read Part 2 of this article series. And if you have questions, feel free to contact us today.
by Sara McCaslin Sara McCaslin No Comments

How to Choose the Right Polymer Seal Material: A Failure-Mode Guide

Most spec sheets are organized by material (PTFE, PEEK, FKM), but almost none are organized by what is actually going wrong in a system. That is backward, since seal failure is the symptom you actually have in hand. 

This failure-mode guide starts from the failure rather than the catalog. This discussion includes seal extrusion, swelling, pressure trapping, wear, and more. For each failure mode, we discuss what it looks like, its root cause, and what to specify for the material.

What Causes Seal Extrusion

Extrusion looks like chunks torn away or flowing into the extrusion gap, usually on the dynamic/pressure side. Extrusion is really a localized case of creep. Under sustained differential pressure, the seal material behaves less like a solid and more like a very slow-moving fluid, flowing into whatever clearance gap it can find. Higher pressure, larger gaps, and higher temperature (which softens the material and accelerates creep) all speed this up. Keep in mind that elastomers have comparatively low creep resistance: under continuous load they keep deforming rather than settling into a stable state, which is exactly what makes them prone to extrusion. 

Thermoplastics like PTFE resist extrusion better than elastomers mainly because they are less elastic, but not because they are immune to creep. Unfilled PTFE, for example, is known for cold flow under sustained load. Filled PTFE compounds (glass, carbon, or bronze) or spring-energized PTFE seal designs are typically specified when extrusion resistance under continuous pressure is the priority. No material choice fully solves an oversized clearance gap; review the design before committing to a material change.

Extrusion and compression set are really two faces of the same creep-driven behavior: one shows up as material flowing away, the other as material failing to recover its shape.

What Causes Seal Compression Set

Compression set is straightforward to spot because it results in a flat-sided cross-section. Compression set results in leakage at low pressure. This can be counterintuitive, because leaks are usually associated with higher pressures. Compression set occurs when a material loses its elastic memory and can no longer rebound over time. It relates to a material’s ability to recover its shape after sustained compression. One fix for compression set is to look for materials engineered for low compression-set values. Also, because compression set develops gradually, it is a good candidate for a preventive replacement schedule rather than reactive repair.

What Causes Seal Hardening / Glazing

Another seal problem is hardening and glazing. When it occurs, the seal will have visible cracking or a glassy/glazed dynamic face, and ties in with a broader loss of elasticity across the whole seal. Two different things can lead to hardening and glazing:

  • Excessive speed that generates frictional heat at the face
  • Fluid/material incompatibility or sustained high fluid temperature

If hardening or glazing is a problem, look for materials with good heat resistance. Confirm actual continuous-use temperature rating (not just peak rating) against real operating conditions, not catalog optimism.

What Causes Seal Swelling

Swelling occurs when a seal loses its molded shape and may appear larger than the spec. Swelling is fluid absorption (water is the most common culprit) or chemical incompatibility. This is a compatibility problem, not a strength problem, so a stronger material is not the fix. Instead, check a chemical-compatibility chart before specifying a material. 

What Causes Seal Scarring

Dents or cuts on the lip of the seal, as well as scratches on the dynamic side, are called scarring. This is usually not a material issue but the result of improper storage, sharp installation tools, or contaminants/scars in the bore or rod. Rather than pursuing a material change, fix the installation practice by supplying proper tools or ensuring the bore is clean, for example. If the scratches can be traced back to contaminated fluid, the system needs flushing. This failure mode does not call for a material or product change.

What Causes Seal Wear

Seal wear is the gradual thinning or degradation concentrated on the seal’s dynamic face, usually from inadequate lubrication or excessive lateral loading. To mitigate premature wear, engineers should consider the friction coefficient and self-lubrication as much as material hardness. The solution to excessive dynamic wear is usually a low-friction, self-lubricating polymer (PTFE, UHMWPE).

What Causes Seal Pressure Trapping and Spiral Failure

Both pressure trapping and spiral failure skew the geometry and design. In pressure trapping, adjacent seals facing the same direction trap fluid, and the fix is a back-pumping design rather than a material change. Spiral failure results when an O-ring twists under long, fast strokes. In this case, the best approach is to fix the geometry (e.g., design a different cross-section) rather than select a new material.

A Seal Decision Framework Quick-Reference

To help you quickly see what to do about the most common seal failure modes, we developed the table below. 

Failure Mode What You’ll Notice Root Cause Material Direction Is This Actually a Design/Install Issue?
Extrusion Chunks torn away or flowing into the clearance gap, usually on the pressure side Creep  – sustained pressure drives the material into the gap over time Filled PTFE (glass/carbon/bronze) or spring-energized PTFE over standard elastomer Partly: oversized clearance gap needs a design review too
Compression Set Flat-sided cross-section; leakage at low pressure Creep-driven loss of elastic memory Material engineered for low compression set No: this is a material property question
Hardening / Glazing Cracking or a glassy dynamic face; general stiffening Frictional heat from speed, or fluid incompatibility/high fluid temp Verify actual continuous-use temp rating vs. real operating conditions Sometimes: check speed/friction before blaming the material
Swelling Soft, shape loss, seal reads larger than spec Fluid absorption (often water) or chemical incompatibility Check chemical-compatibility chart before specifying (nylon is prone) No: compatibility problem, not a strength problem
Scarring Dents/cuts on the lip; scratches on the dynamic side Improper storage, sharp install tools, or contaminated bore/fluid Rarely a material fix Yes: fix installation practice or flush the system first
Wear Gradual thinning concentrated on the dynamic face Inadequate lubrication or excessive lateral loading Low-friction, self-lubricating polymer (PTFE, UHMWPE) Partly: check lubrication/loading alongside material
Pressure Trapping / Spiral Failure Burst at the weaker of two adjacent seals; spiral cuts on an O-ring Same-direction adjacent seals trap fluid; long fast strokes twist the O-ring Rarely the fix Yes: back-pumping design or different cross-section geometry

Application spotlights

In hydraulic and pneumatic cylinders, extrusion and wear are the primary risks with high pressures and high speeds. Swelling, chemical compatibility, and purity requirements are the primary challenges for semiconductor seal applications. In aerospace applications, hardening and compression set driven by wide temperature swings are among the major challenges. Chemical processing seals often face obstacles with regard to swelling and chemical compatibility. 

Conclusion

Seal failures are typically addressed after the fact: a part fails, is replaced in kind, and fails the same way again. The more effective approach is to identify the governing failure mode before specifying a material, not after. Pressure, temperature, chemical exposure, and duty cycle each point to different material requirements; addressing them upfront is more reliable than correcting them after a failure occurs.

For applications where the right material is not clear, our engineering team is available to review your specifications and recommend a solution. Contact us today and let us utilize our knowledge and experience to help you choose the right seal.