by Sara McCaslin Sara McCaslin No Comments

PTFE Auto Molding vs. Machining: When Compression Molding Is the Better Manufacturing Route

Auto molding and machining are are different manufacturing processes that both lead to a finished part. Which option is better depends on part design, production volume, material, critical dimensions, tolerance requirements, production economics, and the equipment in which the part will operate.

In this article, we look specifically at PTFE auto moding and machining to discuss when auto molding is the better manufacturing option.

What Is PTFE Auto Molding?

Auto molding, also known as compression molding, uses heated compression and dies to form a near-net-shape polymer part. It is a commonly used manufacturing technique for making thermoset and thermoplastic parts,  as well as rubber and composites. It is also one of the oldest plastic forming methods still in use. 

The auto molding process starts by placing a pre-measured amount of material (usually in the form of a preheated plug, sheet, or granules) into an open, heated mold cavity. That mold is then closed with a matching upper half. A hydraulic press is used to apply high pressure that forces the material to fill the entire cavity shape. 

The combination of heat (typically 250–400°F depending on the material) and pressure causes the material to cure (or vulcanize). The result is permanent cross-links within the PTFE polymer structure that lock it into the desired shape. For compression molding PTFE compounds, pressure, sintering temperature, and dwell time are critical process variables. Typical molding pressures of 3,000–4,500 psi and sintering temperatures in the 685–720 °F range are required, while the dwell time is dependent on part geometry, volume, and machine capability.

Once curing is complete, which can take anywhere from a minute to several minutes depending on part thickness and material, the mold opens and the finished part is ejected. Auto molded parts often require minimal trimming of excess flash material. 

What PTFE Machining Does Well

An alternative manufacturing method often used with PTFE is machining. Machining removes excess material to produce the final part and may include processes such as milling, turning, and drilling. This approach is well adapted to situations that involve …

  • Prototype and development parts
  • Low-volume production
  • Designs that are still changing
  • Components with highly localized geometry or features
  • Parts requiring final sizing, precision finishing, or secondary features after molding
  • Jobs where a dedicated mold is not economically justified

A part’s complexity, stock availability, scrap rate, and tolerance demands all impact the cost of machining PTFE parts.
Where Auto Molding Excels Over Machining

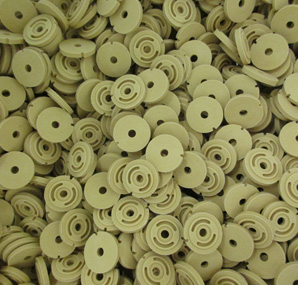
There are, however, several benefits to auto molding. For example, near-net-shape production can reduce material removal and tooling can make sense when demand is stable and sufficient. Auto molding is also a  repeatable molding process can support recurring production. 

And thick, large, or geometry-specific parts may benefit from being formed closer to finished shape. In addition, molding can reduce subsequent machining, though some finishing may still be required (e.g.,  machining, facing, drilling, or other finishing operations. Finally, material and process control can be tailored to the specific PTFE compound and part geometry

What are the Real Decision Factors

The table below summarizes the decision factors that are involved.

PTFE Auto Molding vs. Machining: Decision Matrix

Decision Factor PTFE Auto Molding Favored When Machining Favored When
Production Demand The part is recurring, and annual demand supports tooling economics. Demand is low, uncertain, or one-time.
Geometry Near-net-shape tooling can form much of the required profile. Geometry changes frequently or needs flexible revision.
Material Utilization Starting from stock would create substantial removed material. Stock shape is already efficient for the design.
Lead Time Tooling exists or production is repeatable after tool qualification. A part is needed before a tool can be designed and qualified.
Tolerances The molded shape can meet requirements with limited finishing. Tight, localized, or feature-specific tolerances dominate.
Secondary Operations The design can be completed with minimal post-mold work. Numerous holes, threads, grooves, or custom features are required.
Design Maturity The drawing, material, and demand forecast are stable. The part remains in prototype or iterative design stages.

PTFE Compound Selection Is Part of the Auto Molding Process Decision

Keep in mind that unfilled PTFE and filled PTFE compounds should not be treated as interchangeable. For example, fillers can impact properties such as wear resistance, stiffness, thermal behavior, electrical behavior, friction, and process response. The compound selected should account for factors such as pressure, sliding speed, counterface, media, temperature, chemical exposure, contamination, and dimensional requirements. A manufacturing route should be selected after the material and functional design are understood, not before.

What to Send a PTFE Auto Molder

Here is the type of information that a PTFE molder would need to provide a quote:

  • Part drawing and revision level
  • 3D model if available
  • Material specification or functional requirements
  • Critical dimensions and GD&T (Geometric Dimensioning and Tolerancing)
  • Tolerances required after sintering and any machining
  • Service temperature, pressure, media, and load conditions
  • Counterface materials and surface finish for bearing or sealing components
  • Regulatory, traceability, inspection, or documentation requirements
  • Whether the part is a prototype, bridge-production part, or long-term production design

Conclusion

PTFE auto molding shapes near-net parts under heat and pressure, which both cuts waste and machining time versus starting from stock. Auto molding is the smart choice for recurring, stable-volume production where the molded shape can meet tolerances with minimal finishing; machining, however, is till the preferred choice for prototypes, low-volume runs, or tight localized features.

Not sure which route best fits your part? Send Advanced EMC your drawing, material spec, critical dimensions, and production volume, and our team will help you find the most cost-effective path from design to finished part.

by Daniel Mays Daniel Mays No Comments

Machined and Molded Polymer Bearings: Nylon 66, PEEK, and PPS

Nylon 66, PEEK, and PPS are available in bearing grades, but how should they be manufactured? The choice of manufacturing method can have a significant impact on their tolerances, performance, and cost. 

This blog post focuses on machined and molded polymer bearings, including their benefits and limits, how they compare to metal options, and the best ways of manufacturing bearings made from three very different materials: Nylon 66, PEEK, and PPS. 

Introduction to Polymer Bearings

Polymer bearings are low-friction, lightweight alternatives to traditional bearings. They are corrosion-resistant and offer varying degrees of chemical resistance. Polymer bearings are also known for their ability to run dry or with minimal lubrication, as well as good wear characteristics. They are also electrically insulating and offer quieter operation than their metal counterparts.

However, polymer bearings do have their limits. They are more susceptible to thermal expansion and may have lower load limits and PV than their metal counterparts, but the addition of fillers can mitigate this issue. In some cases, they may be susceptible to moisture uptake. 

The table below summarizes the major differences between metal and polymer bearings.

Metal vs Polymer Bearings

FeatureMetal BearingsPolymer Bearings
FrictionLow only with lubricationLow due to inherent lubricity
LubricationRequiredOften not required
Wear MechanismAbrasive/adhesive fatigueTransfer film formation
CorrosionPossibleNearly immune
Shock/VibrationNo dampingNatural damping
SpeedHighModerate
LoadHigherModerate
Temperature LimitsExcellentVaries by polymer
MaintenanceHigherVery low

Machined vs. Molded Polymer Bearings

Machined bearings are best for small production runs where tight tolerances and complex geometries are involved, and machining is ideal for prototypes, custom components, and specialty rotating equipment. This approach to manufacturing bearings also allows the material to remain homogenous with no molded-in stresses.

Molded bearings are the best option for high-volume production, and they are more cost-effective for simpler geometries. Molding also means reduced part-to-part variation; however, molded-in stress may be present, and there are limits to surface finish.

When choosing between machined and molded polymer bearings, the key factors are:

  • Geometry
  • Tolerances
  • Cost
  • Production volume

Nylon 66, PEEK, and PPS

Among the various options for polymer bearings are Nylon 66, PPS, and PEEK. The table below summarizes the differences between these materials.

Performance Comparison: Nylon 66 vs. PPS vs. PEEK

Property / FactorNylon 66PPSPEEK
Max Continuous Use Temperature~100–120°C~200–220°C~240–260°C
Wear ResistanceGood (improved with lubrication)Very goodExcellent (especially filled grades)
FrictionLowLowVery low
Moisture AbsorptionHigh (can swell, affects tolerances)Very lowVery low
Dimensional StabilityModerate (affected by humidity)HighVery high
Chemical ResistanceModerateExcellentExcellent
Mechanical StrengthGoodHighVery high
Impact ResistanceVery goodModerateGood
Creep ResistanceModerateGoodExcellent
PV CapabilityLow–MediumMedium–HighHigh–Very High
CostLowMediumHigh
Machining SuitabilityExcellentExcellentExcellent (best with filled grades)
MoldabilityExcellentGoodGood
Typical ApplicationsRollers, appliance bearings, automotive interior componentsPumps, compressors, chemical processing, precision housingsAerospace, oil & gas, high-speed bearings, semiconductor tools

Manufacturing Nylon 66, PEEK, and PPS Bearings

There are several different bearing materials available, but of interest in this blog post are Nylon 66, PPS, and PEEK bearings.

Nylon 66

Nylon 66 is very easy to mold because of its low viscosity, forging processing window, and good flow characteristics. However, there is going to be high mold shrinkage, which requires careful part design to keep warpage under control. Nylon also absorbs moisture, which means that drying is important before molding takes place. 

Nylon also machines easily, but its high ductility leads to stringy chips that necessitate the use of chip-breakers. Heat buildup is also an issue with nylon, and moisture absorption can impact the level of precision that can be achieved. It does, however, respond well to secondary machining on already molded parts, but does not work well with tight-tolerance CNC components.

PEEK

Because PEEK high a high melt temperature around 343°C, a very narrow thermal window that requires precision temperature control, and requires a heated mold, it is considered challenging to mold. However, with the right processing parameters and careful design, PPS can be molded and can manufacture parts with excellent thermal and mechanical performance (but is more expensive). 

PEEK is very difficult to machine. Its high modulus and hardness make it especially tough on cutting tools, and reinforced grades can be highly abrasive. It also generates an abundance of heat, thus requiring the use of coolants. However, machining PEEK supports excellent tolerances and surface finishes when the right combination of feed and speed is used. In fact, PEEK is frequently machined for low-volume aerospace and medical components.

PPS

PPS is not as easy to mold as Nylon 66 because its melt temperature is higher, it possesses a narrower processing window, and has high viscosity. However, it does exhibit very low shrinkage and excellent dimensional stability. PPS molding is very predictable and an excellent option once the right processing parameters have been figured out.

PPS is machinable, definitely more so than Nylon, but tends to be more brittle. It produces short chips and there is a risk of edge chipping during more aggressive cuts. On the other hand, it is good for tight tolerances. Note that filled grades of PPS can accelerate tool wear. Machining PPS is ideal for high-precision parts where dimensional stability is important.

Conclusion

Machined and molded Nylon 66, PPS, and PEEK bearings continue to gain traction because of properties such as low friction, wear characteristics, damping, corrosion resistance, and chemical compatibility. If you are in need of polymer bearings, Advanced EMC is here to help. Our team of engineers and bearing experts can help you from initial design to manufacturing to testing. Contact us today to learn more.