
The HVAC/refrigeration industry in the US is still in the midst of transitioning to A2L refrigerants (R-454B, R-32, etc.) that replace R-410A. These changes are required as part of the Environmental Protection Agency’s AIM Act and its mandate of a stepped phasedown reaching 40% below baseline by 2024 and 85% by 2036. This has forced HVAC manufacturers to shift away from R-410A to lower-GWP alternatives.
And with that shift has come some surprising seal failures. A piece of HVAC equipment that has worked for 15 years starts experiencing seal leaks, hardening, or swelling for the first time. This is a serious compatibility issue between low-GWP refrigerants and traditional sealing solutions.
This article looks at the causes behind these failures, the failure modes involved, and seal materials to consider in solving these issues.
A Chemistry Lesson
The mechanisms behind the new seal failures occurring with low-GWP A2L refrigerants can be explained with some rather basic chemistry.
Loss of the R-125 Buffer
When swapping R-410A (a 50/50 blend of R-32 and R-125) for R-454B (68.9% R-32 / 31.1% R-1234yf) or pure R-32, the solvent properties of the working fluid change significantly. R-125 acted as a flammability suppressant and modified the polar solvency of the mixture.
Next-generation A2L blends like R-454B remove R-125 entirely, and R-1234yf is itself a smaller, more polar molecule than R-125. The shift, then, is not just R-125’s absence, but also R-1234yf’s more aggressive solvency actively driving elastomer attack. The result of switching to A2Ls has been significantly higher fluid solvency against elastomers than R-410A produced.
Enhanced Polymer Penetration
Higher concentrations of R-32 and fluorinated alkenes (HFOs) exhibit smaller molecular sizes and higher dipole interactions, increasing their diffusion rates into elastomeric matrices.
Polyolester (POE) & Polyvinyl Ether (PVE) Synergy
In addition, A2L refrigerants in US systems typically rely on Polyolester (POE) oils. The refrigerant lowers the viscosity of the oil and enhances its ability to penetrate elastomer matrix structures. As a result, the seal fails not from the gas alone, but from the combined refrigerant-oil working fluid.
The Three Primary Failure Modes
There are three failure modes associated with the chemical reactions just discussed: gland overfill, post-maintenance leak, and RGD (Rapid Gas Decompression).
Excessive Swell / Gland Fill-Ratio Exceedance
Overfilled seal glands, regardless of cause, lead to issues with extrusion into clearances, increased friction on dynamic shafts/spools, nibbling, and permanent mechanical tearing. This may initially appear as a lubrication issue, but it is not. The polymer matrix is absorbing the refrigerant/oil mixture, causing volume expansions exceeding 15–20%. Note that the seal was correctly sized and installed. The volume growth occuring afterward is from chemical absorption, not from an installation or specification error.
The “Post-Maintenance” Leak
As refrigerant permeates the seal, it leaches out the low-molecular-weight plasticizers, processing aids, and cross-linking agents from the elastomer. When this happens under system pressure, the seal appears tight because of swell. However, once the system is evacuated, vented, or cycled off, the absorbed refrigerant off-gasses from the seals. This off-gassing leaves behind an elastomer that has lost volume. The seal then shrinks below its original dimensions, losing compression set and causing sudden leaks.
Rapid Gas Decompression (RGD)
Next is RGD, which is a well-established failure mode in high-pressure gas sealing (e.g., API 6A, NORSOK M-710 test protocols) that A2L refrigerants newly expose HVAC seals to because of their smaller molecular size and higher solubility. In short, A2L molecules are able to permeate high-pressure elastomeric seals. During a rapid system pump-down or sudden pressure drop, the gas trapped inside the elastomer pores expands faster than it can diffuse out. The result of RGD is internal blistering, micro-fissures, and catastrophic seal rupture from the inside out.
Compatibility is at the Core
A2L systems commonly pair with different POE oil formulations than their A1 predecessors. It is, however, key to remember that the oil in A2L refrigerants is just as much a part of the compatibility question as the refrigerant itself. Testing a seal compound against R-454B alone while ignoring the oil is only testing half the problem.
Seal Material Considerations
The information below summarizes the most commonly used materials for HVAC seals and their performance for both R140A and A2L refrigerants.
| Sealing Material | R-410A Compatibility | A2L (R-454B / R-32) Rating | Primary Risk & Failure Mechanisms | Engineering Recommendation |
|---|---|---|---|---|
| NBR (Nitrile) | Acceptable Baseline (known long-term POE extraction risk) | HIGH RISK | High extraction of plasticizers; severe shrinkage post-evacuation. Swell varies unpredictably with ACN content. | Not Recommended. Replace with peroxide-cured FKM or PTFE. |
| HNBR (Hydrogenated Nitrile) | Good / Excellent | MODERATE TO HIGH | High swell with low-ACN grades; low-temperature flexibility loss with high-ACN grades. | Requires rigorous validation per compound formulation. |
| FKM (Standard Bisphenol-Cured) | Standard Choice | CONDITIONAL | Vulnerable to chemical attack by basic additives/amines in PVE oils and polar A2L mixtures. | Avoid standard grades. Use low-swell peroxide-cured FKMs. |
| FKM (High-Fluorine / Peroxide-Cured) | Excellent | GOOD | Significantly reduced swell and chemical resistance against POE/PVE mixtures. | Recommended for static O-rings requiring elasticity. |
| EPDM* | Specialty Use | SEVERE FAILURE | Incompatible with synthetic POE/PVE lubricants, causing immediate degradation and extreme swell. | Prohibited in POE/PVE lubricated systems. |
| PTFE / Virgin & Filled PTFE** | Premium / Inert | EXCELLENT (BEST PRACTICE) | Zero chemical absorption, zero swell, zero plasticizer extraction, immune to RGD. | Best Practice. Ideal for dynamic rotary shaft seals and control valves. |
| Fluorosint® 500 PTFE** | Premium / Inert | EXCELLENT (BEST PRACTICE) | Synthetic mica-filled PTFE; virtually immune to RGD, chemical swell, and leaching. | Superior Choice. Offers lower thermal expansion and greater deformation resistance than standard PTFE under heavy load. |
| Fluorolon 1065** | Premium / Inert | EXCELLENT (BEST PRACTICE) | Modified PTFE compound with high chemical inertness and zero extraction risk. | Cost-effective alternative to standard virgin/filled PTFE for aggressive A2L and lubricant environments. |
| Polyketone (PK)** | Good | EXCELLENT | Rigid semi-crystalline thermoplastic; non-porous structure eliminates RGD and plasticizer leaching. | Eco-friendly engineering option. High wear and impact strength; best suited for anti-extrusion back-up rings or structural seal components. |
| PVDF (Kynar®)** | Good | EXCELLENT | High mechanical strength and creep resistance; resistant to chemically aggressive refrigerants. | Recyclable engineering polymer. Ideal for rigid back-up rings, valve seats, and high-pressure containment components. |
*Note on EPDM: This incompatibility predates the A2L transition and applies to ester-based lubricants generally, not to the A2L refrigerant molecule itself.
**Thermoplastic options (PTFE, Fluorosint, Fluorolon, Polyketone, PVDF) are not elastomers and are not drop-in replacements in standard elastomeric O-ring grooves. They typically require redesign (e.g., spring-energized lip seals) or are used as backup/anti-extrusion rings.
Conclusion
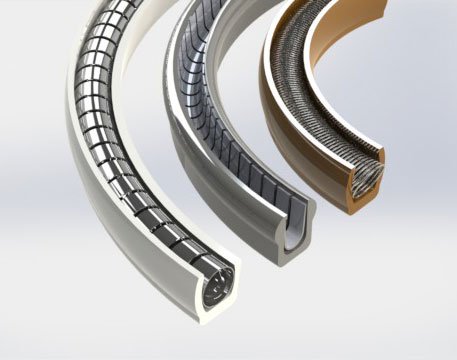
As legacy systems are retrofitted for use with A2L refrigerants, it is important to consider the compatibility of both the refrigerant and its oils with the seal materials. If you are looking for an effective seal design that is resistant to the harmful effects of A2L refrigerants, talk to the seal experts at Advanced EMC. Our team is familiar with HVAC / Refrigeration seal needs and is ready to work with you from design to installation and beyond.